Barrels and screws
Reiloy Screws
Custom wear-protected screws up to 9 m long
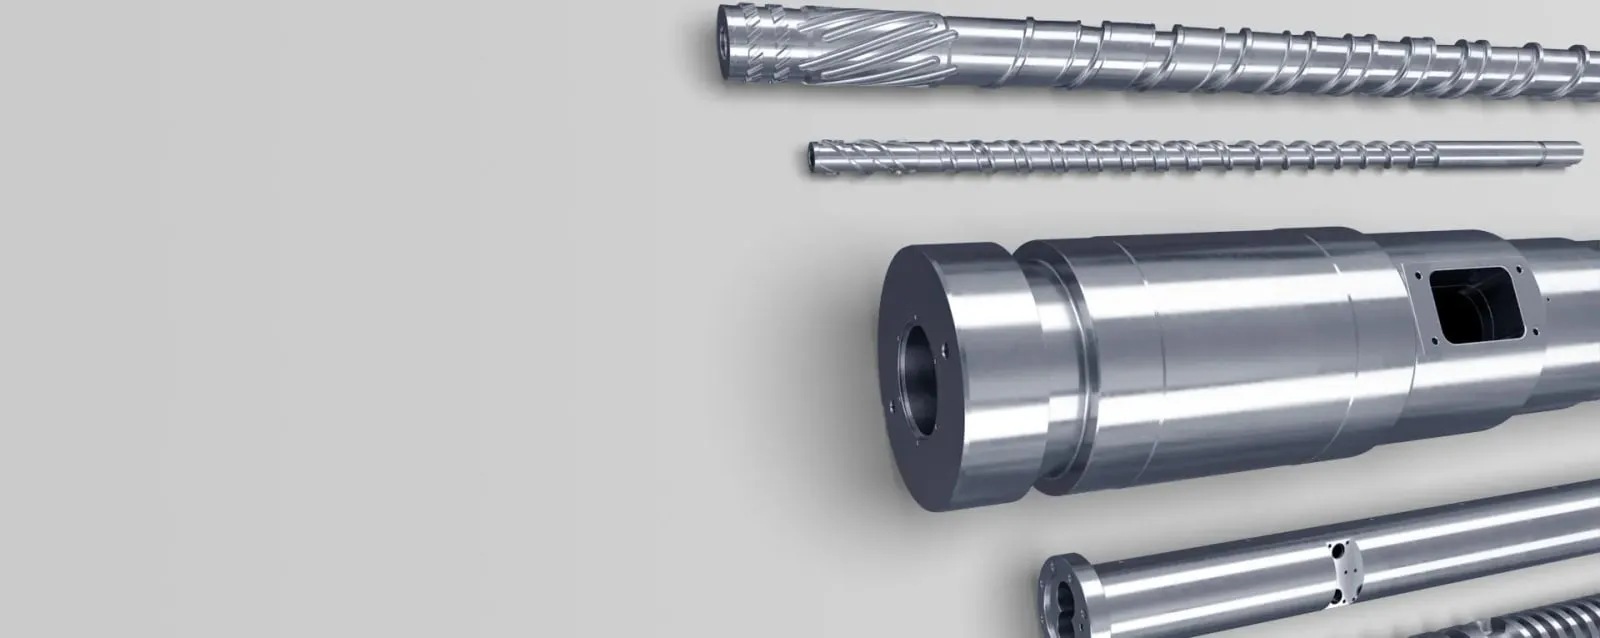
Reiloy screws for extrusion and injection moulding combine an application-specific geometry, wear protection and a suitable material pairing with the barrel. They are manufactured in diameters of 40–300 mm and lengths of up to 9 m in Smart, Advanced, Premium and Select versions.
Benefits
- Hard alloys developed and produced in-house
- Screw geometry tailored to the application, optimal barrel/screw combination
- Long maintenance intervals
- Screw lengths up to 9 m
- ReiMix-HS: up to 3× better mixing effect than a spiral shear section
- Series production to customer drawings
- Quality to DIN EN ISO 9001:2015
Applications:
- Extruder plasticizing units
- Injection moulding machine plasticizing units
- Processing of filled and abrasive plastics
- Fluoropolymers (PTFE, FEP)
We supply the equipment configured for your application. In your inquiry, please state the material processed, the required throughput and the line parameters – we will prepare a tailored quotation.
Need help choosing? Call us on +420 571 647 228 or write to info@azurr-tech.cz.
Technical data
| Screw diameter | 40–300 mm |
|---|---|
| Length | max. 9,000 mm |
| Surface treatment | plasma or gas nitriding, hard chrome, PVD |
| Nitriding steel (Smart) – surface hardness | 900–1 100 HV5 |
| R331 / R341 – hardness | min. 56 HRC |
| R331 / R341 – composition | vanadium carbides, Cr; iron-based martensitic alloy |
| RS12 – hardness | min. 45 HRC |
| RS12 – main alloying elements | Cr, W |
Description
Reiloy manufactures ready-to-install screws to the customer's drawing or with its own geometry design. It develops and produces the hard alloys for hardfacing in-house and cooperates with machine builders, raw material manufacturers and universities.
Insufficient wear protection leads to material loss on the screw and barrel, internal leakage and process fluctuations. The choice of version is therefore based on the filler content and abrasiveness of the processed material.
The optional ReiMix-HS mixing element improves the mixing effect up to threefold compared with a spiral shear section and can be used in both extrusion and injection moulding.
Optional equipment
More products in this category
Barrels and screws